
From printing and material handling to bag making and final inspection, we stay close to every step. With more than 22 years of manufacturing experience, we keep improving our equipment, processes and quality control to make packaging that is consistent, reliable and ready for real production.
view our story
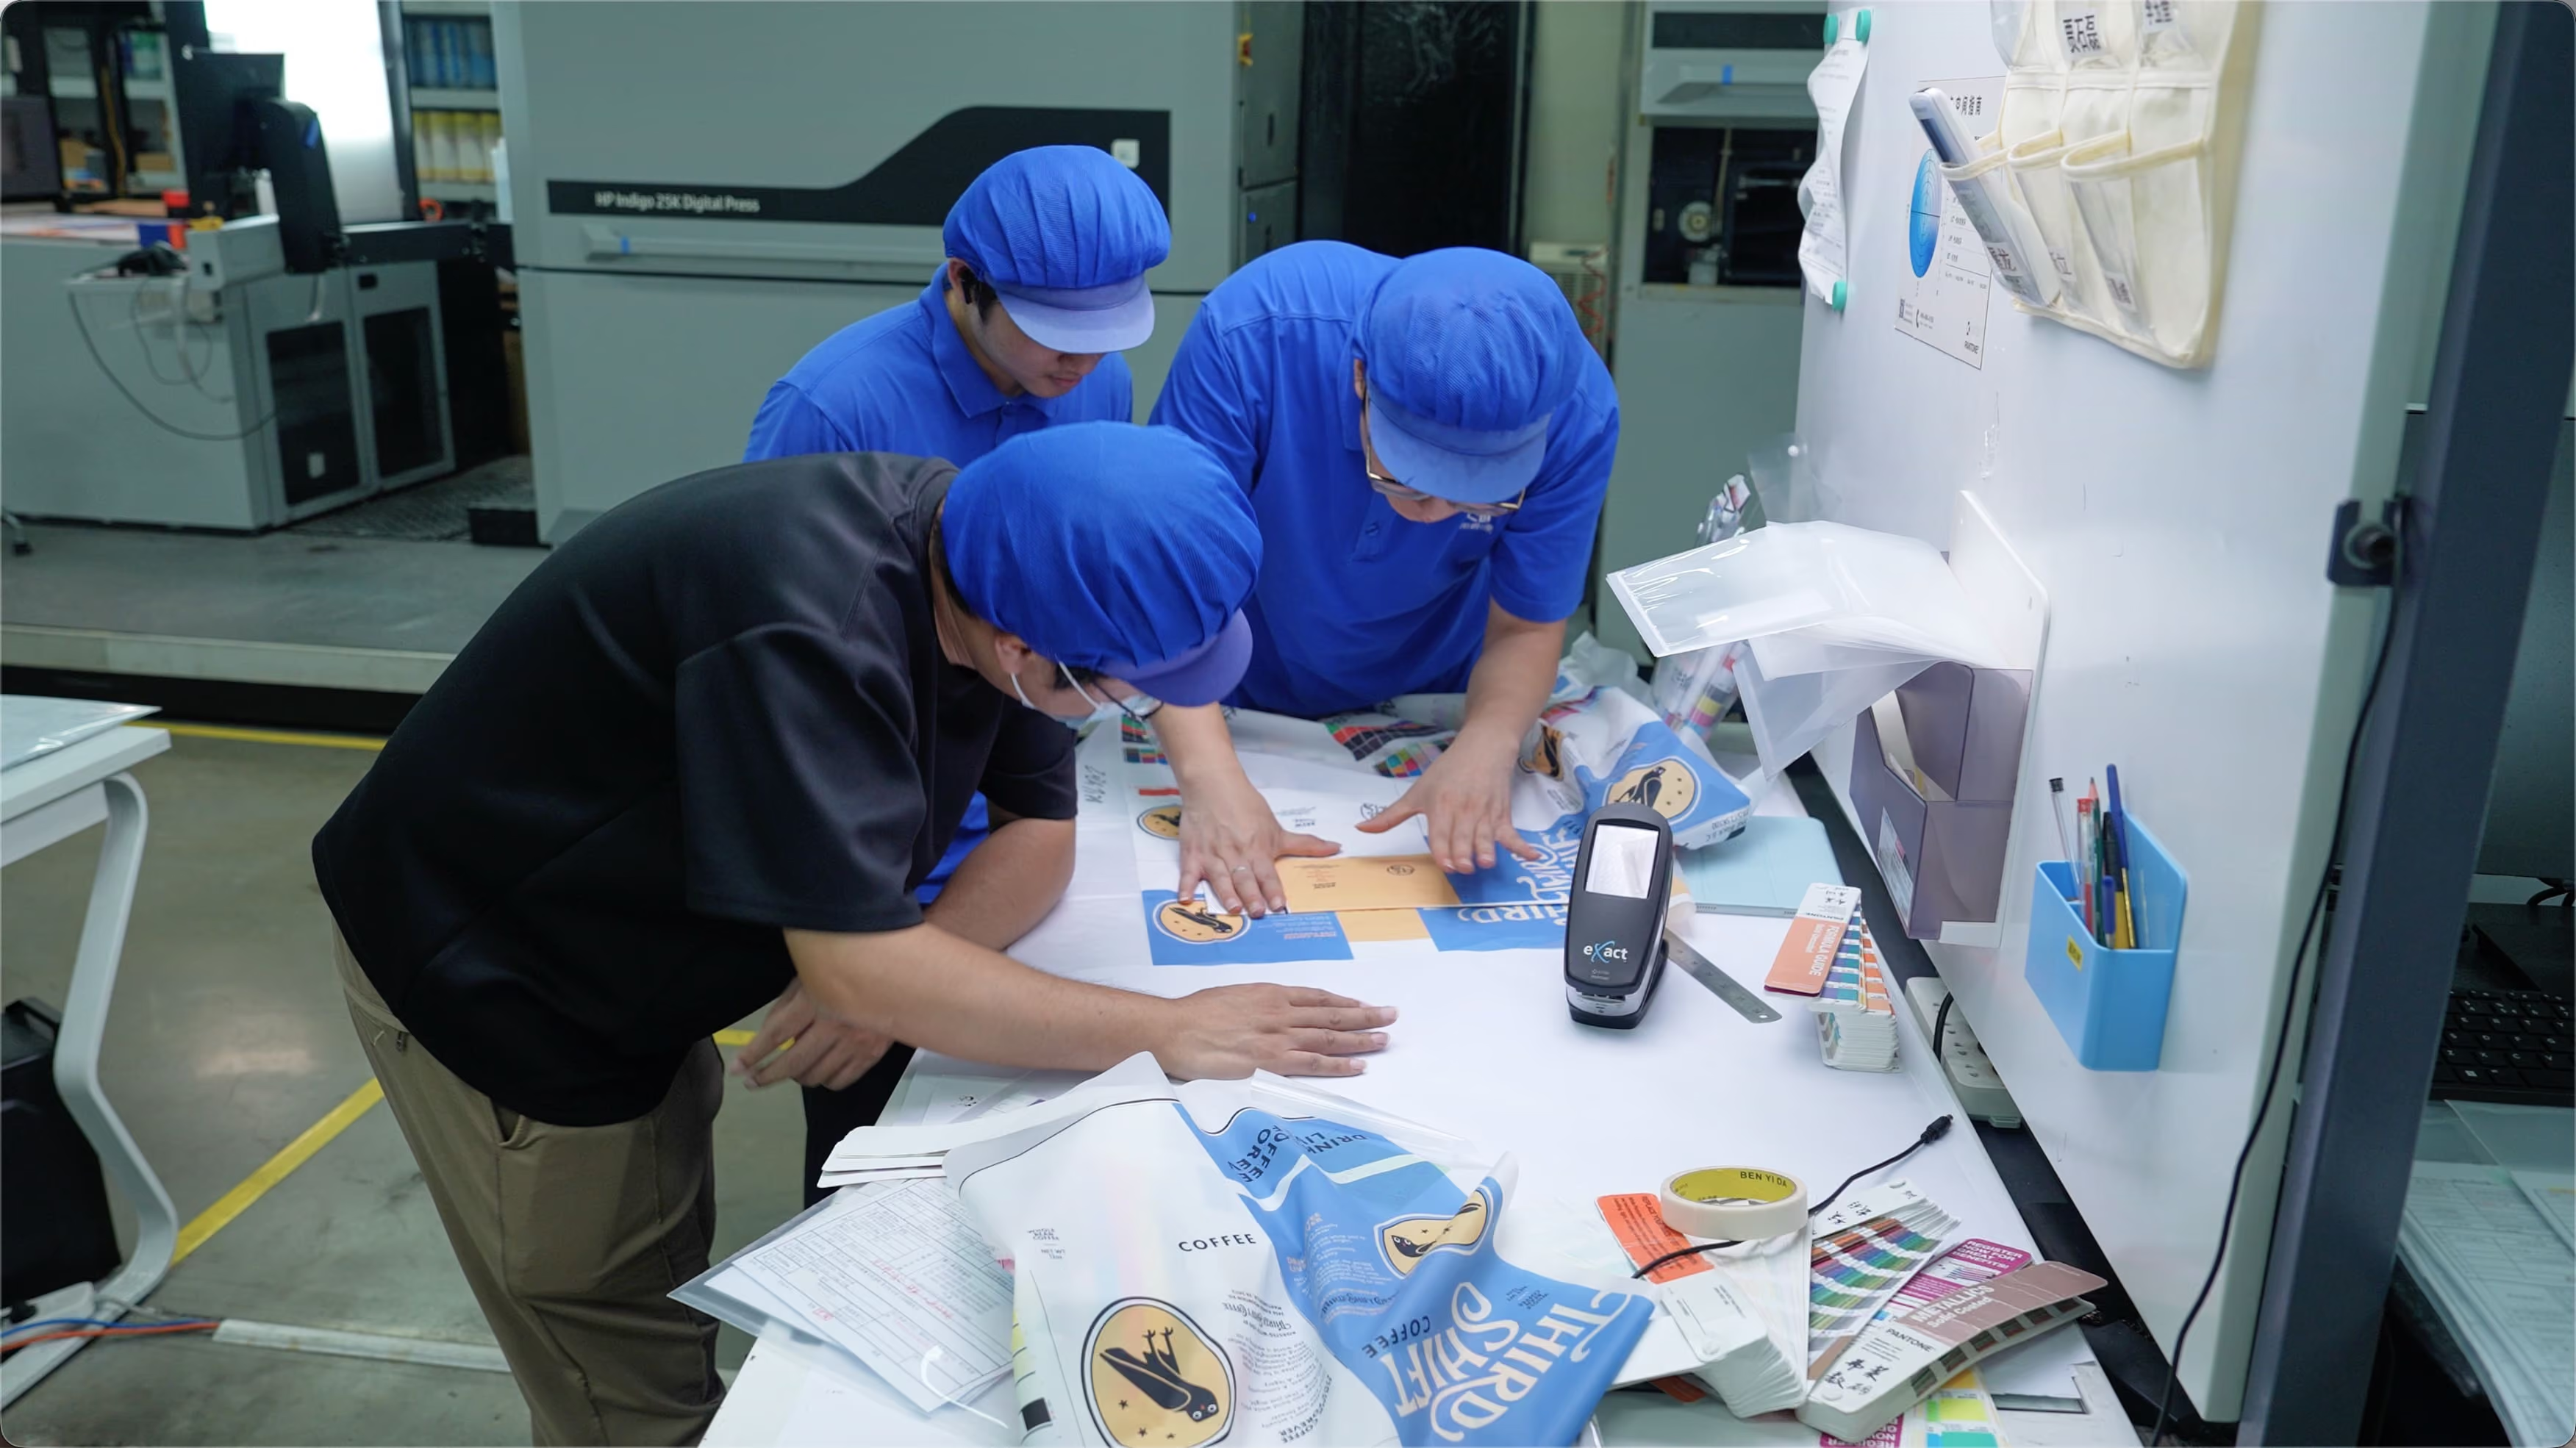
For Third Shift, the colors were already very close to the target on our first print.
We then made six rounds of fine adjustments to hue, chroma, and lightness, using CIELAB and ΔE measurements to ensure the final colors were accurate and consistent.

BAD Coffee’s packaging is produced on our traditional bag-making line.
We carefully process the film, heat-seal it, and cut it into finished bags, while closely controlling the sealing temperature and film tension to ensure consistent quality across every bag.

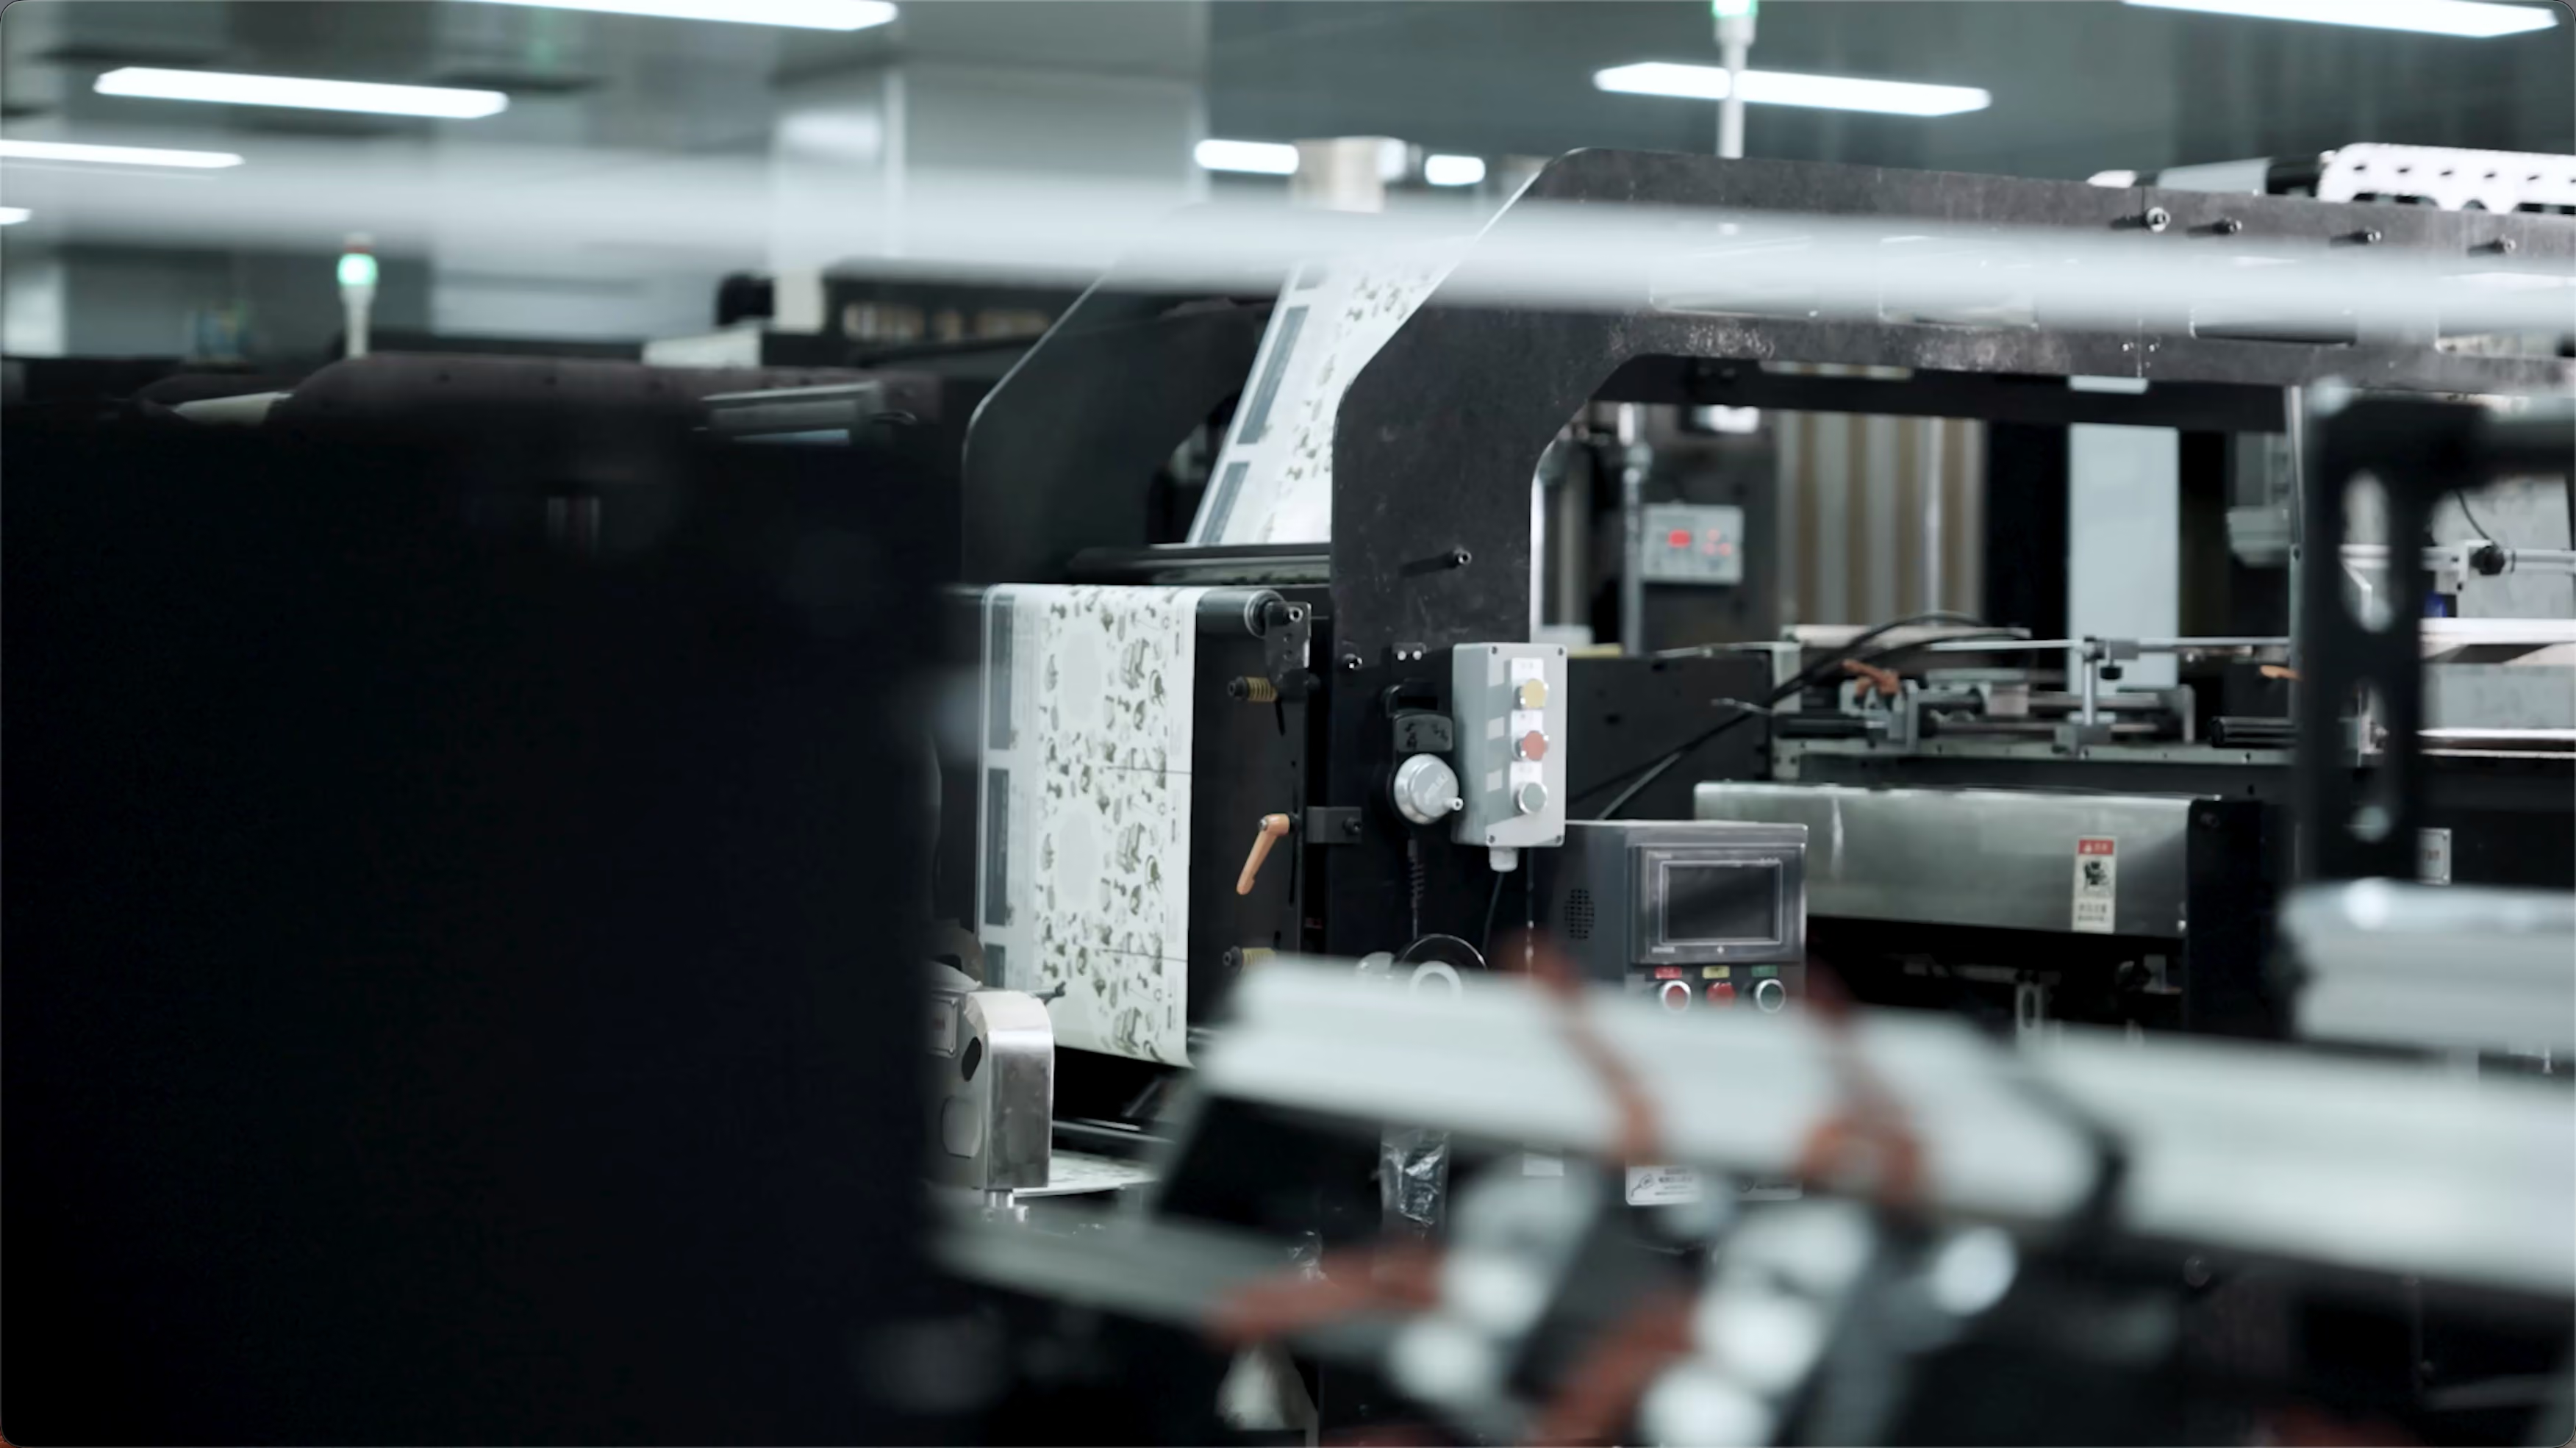
For Stooker, we use rotogravure printing for large-volume production. Each color is printed separately, allowing us to achieve sharp details and consistent colors across large areas.
Throughout the printing process, we carefully monitor color matching to ensure every bag meets the same standards.
Before production, we check paper weight, thickness, and moisture; film thickness, coefficient of friction (COF), and barrier properties (OTR and WVTR); as well as ink viscosity and color.
All materials are inspected using AQL 2.5 sampling. Materials that fail inspection are not used.
During production, we regularly check print alignment, color accuracy (Delta E), lamination strength, seal quality, and packaging dimensions.
All results are recorded, and any issues are addressed promptly.
Finished packaging is inspected using AQL 1.5 sampling.
We check appearance and color under D65 standard lighting, and test seal strength, tear resistance, and zipper performance.
We keep samples from every production batch for 12 months.
We record material batches, production operators, inspection results, and corrective actions, so every stage of production can be traced.
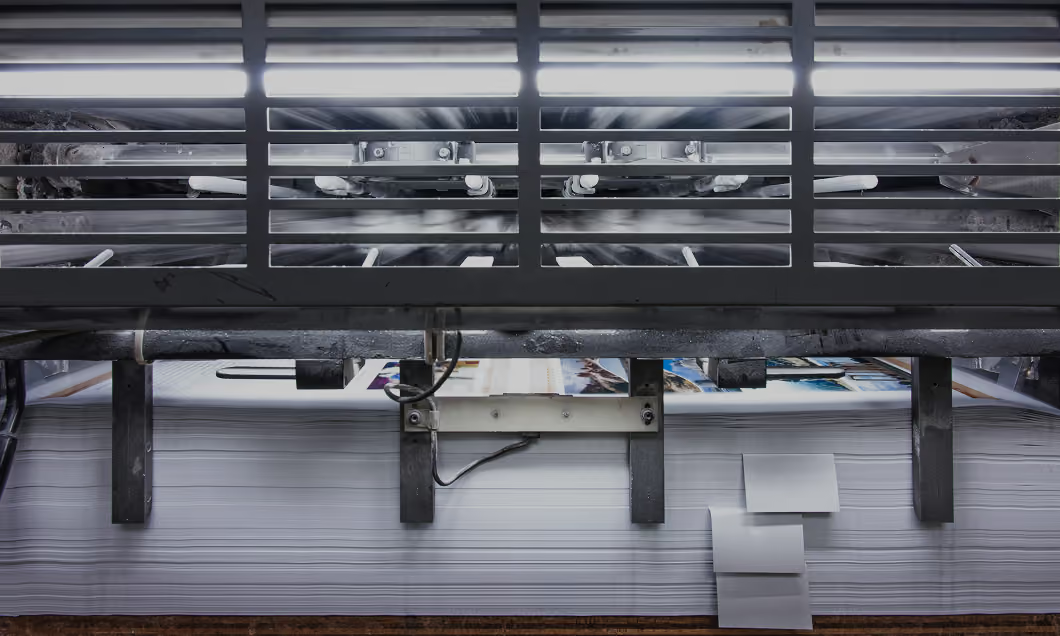
Flexographic printing uses flexible printing plates to produce sharp graphics and consistent colors, making it a reliable choice for a wide range of flexible packaging.
MOQ: 10,000+ pcs
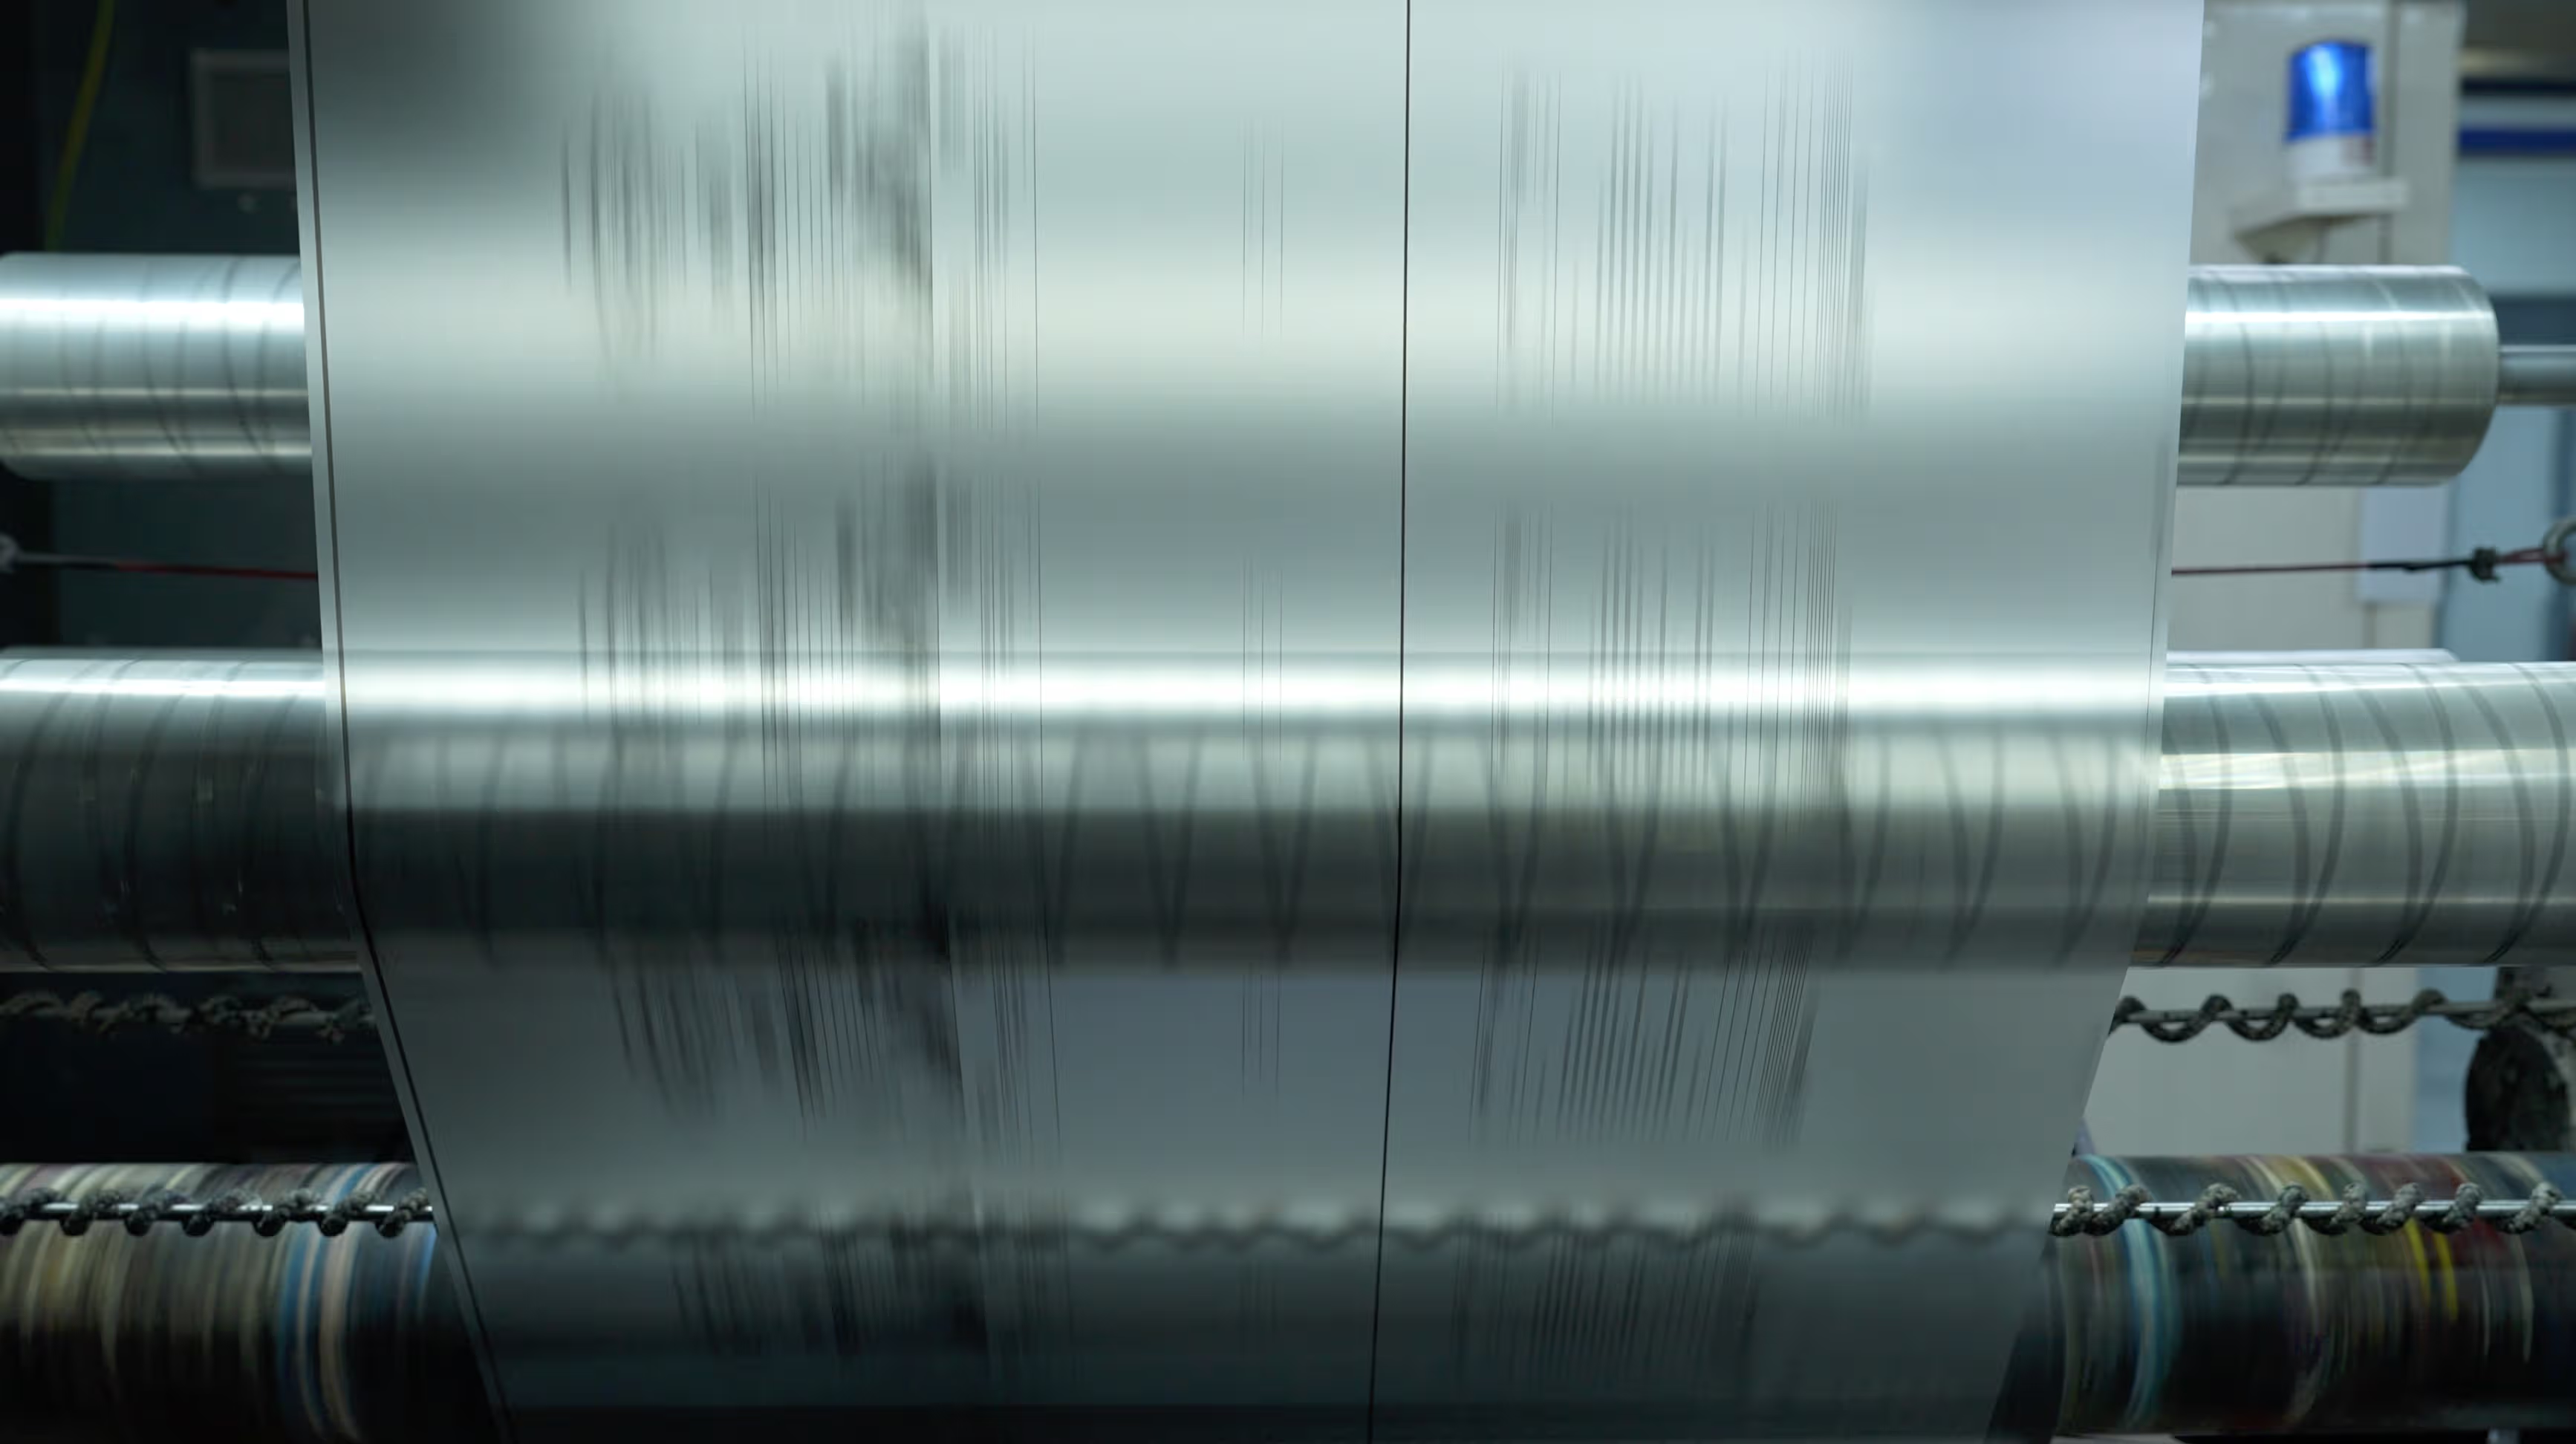
Best for large runs with stable, high-quality colour reproduction.
Requires printing plates.
MOQ: 10,000+ pcs | Prodution time: 6-7 weeks
Ideal for smaller runs, quick sampling, and flexible designs.
MOQ: 3,000+ pcs | Prodution time: 5-6 weeks
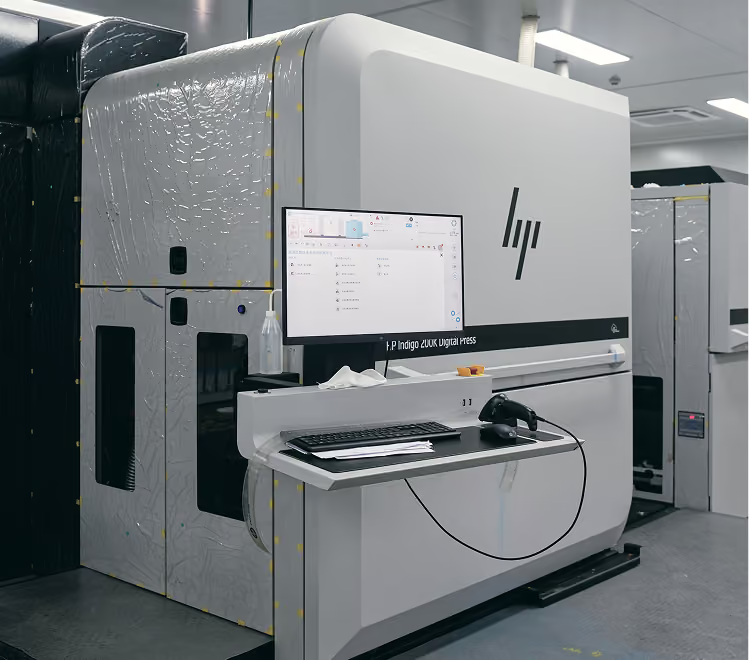
At Holden Pak, we continue to upgrade our equipment to improve print quality and production consistency.
The HP Indigo 200K is used for flexible packaging where colour accuracy and detail matter. With LEP and One Shot Color technology, multiple colour separations are transferred together to improve registration and consistency.
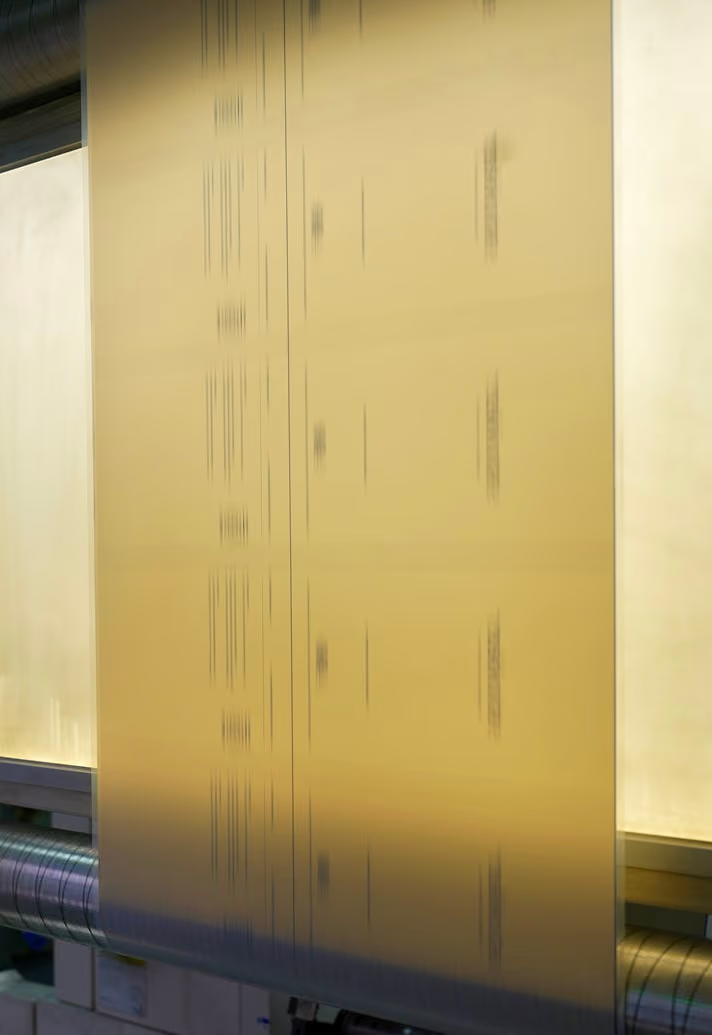

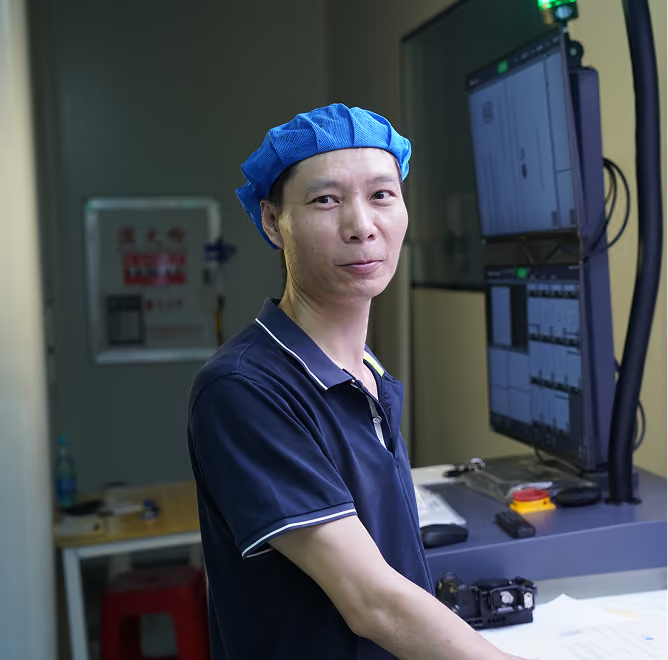
During production, we inspect every active production line every 2 hours. We check packaging dimensions, print alignment, color accuracy (Delta E), lamination strength, and seal integrity.
If we find any issues, we make adjustments to the printing process, and any packaging that fails inspection is rejected.
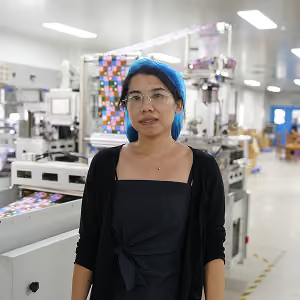
“I’m responsible for keeping the line on schedule and making sure each process follows the approved production standard.
We check material setup, machine settings, sealing quality and in-line QC during the run. If we see a deviation, we stop and fix it before it moves to the next stage. The goal is to keep every batch consistent from start to finish.”
“Before the bags leave the factory, we check the quantity, appearance and packing. Small details matter, especially when thousands of bags are going to the customer.”
“Colour can look different on different materials, so we check it carefully during production. The goal is simple: make sure the finished pack looks like the approved sample.”



We’ll reply within 24 hours to confirm the details and help with your quote.